|
Product Details:
Payment & Shipping Terms:
|
| Max Product Volume: | 10 L | Number Of Die Heads: | 1, 2, 3, 4 |
|---|---|---|---|
| Screw Diameter: | 80 Mm (L/D 24) | HDPE Plasticizing Capacity: | 90 Kg/h |
| Clamping Force: | 150 KN | Control System: | PLC With Touch Screen |
| Applicable Materials: | PE, PP, PVC, PA | Station: | Double |
| Highlight: | Extrusion Blow Molder 10L Bottles,Four Head Extrusion Molding Machine,Chemical Bottle Extrusion Blow Molder |
||
Chemical packaging punishes weak bottles. A 10 litre container filled with caustic or solvent needs a consistent wall at the shoulder and a neck finish that seals, and both come from a stable parison and a clamp that does not breathe during blow-up.
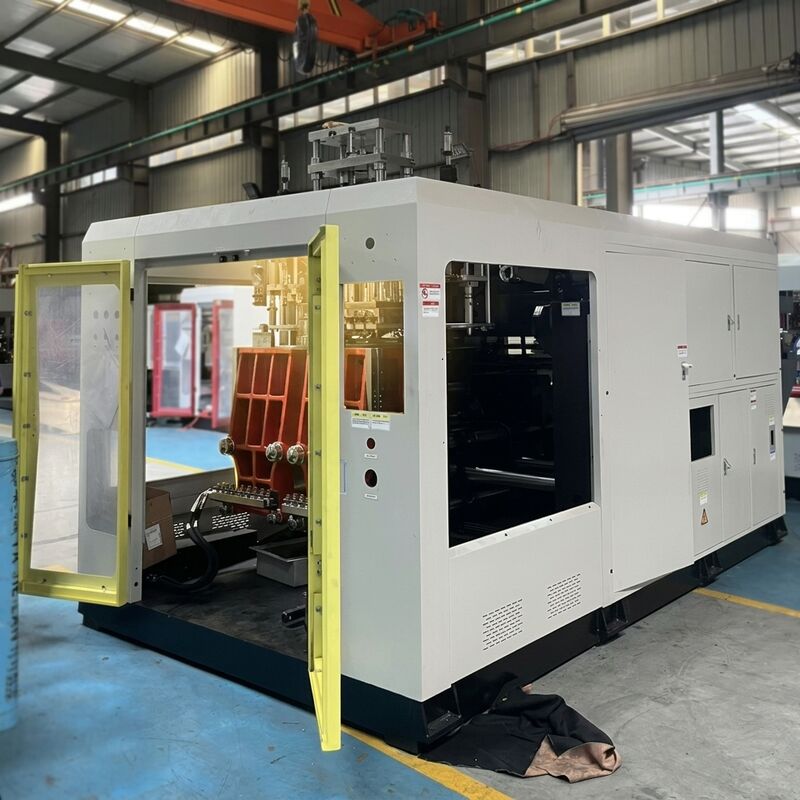
The MP80D is configured for that duty: 150 kN clamp on a 520 x 460 mm platen, an 80 mm screw feeding 90 kg/h of HDPE, and optional multi-layer die heads if a barrier structure is needed for solvent based products.
Key Features| Parameter | MP80D Specification |
|---|---|
| Applicable materials | PE, PP, PVC, PA |
| Max product volume | 10 L |
| Number of die heads | 1, 2, 3, 4 |
| Clamping force | 150 kN |
| Platen opening stroke | 220 - 620 mm |
| Max mould size (W x H) | 520 x 460 mm |
| Screw diameter | 80 mm |
| Screw L/D ratio | 24 |
| HDPE plasticizing capacity | 90 kg/h |
| Screw heating | 4 zones, 15.85 kW |
| Die head heating | 3 zones, 10 kW |
| Extrusion motor power | 30 kW |
| Oil pump motor power | 18.7 kW |
| Total installed power | 80 kW |
| Cooling water consumption | 40 L/min |
| Compressed air | 1.5 m3/min at 0.6-0.8 MPa |
| Machine weight | 8.2 t |
| Machine dimensions (L x W x H) | 4.0 x 2.3 x 2.5 m |
A: Yes, with a multi-layer die head. A barrier layer such as PA or EVOH is co-extruded inside the HDPE wall, and the layer proportion is set through the head flow plates and verified by sectioning the first samples.
Q: What wall thickness do chemical containers need?A: Most 10 litre chemical containers run 2 to 3 mm depending on drop test requirements and the filling temperature. We tune it on your mould during the factory trial and record the setting in the recipe.
Q: Is the neck finish accurate enough for a sealing cap?A: Neck geometry comes from the mould, but machine stability decides whether it is repeatable. The 150 kN clamp and stiff 8.2 tonne frame keep the neck round, which is the usual cause of leaking caps on chemical bottles.
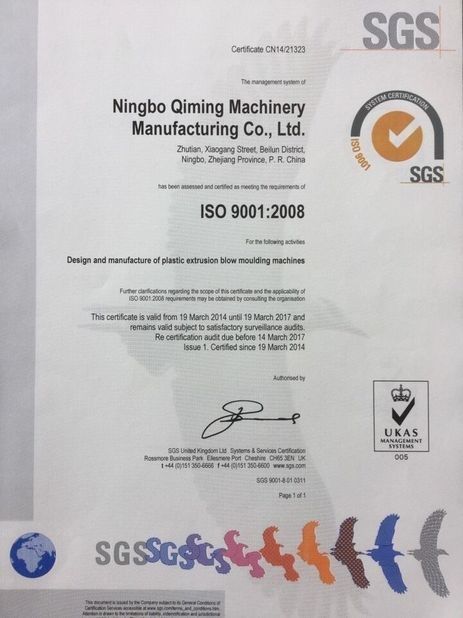
Packaging, Delivery and Quality AssuranceThe machine is shipped with anti-rust protection on all machined surfaces in an export wooden case with steel reinforcement and moisture barrier film. Delivery is 25 to 35 working days after deposit. CE marking, ISO9001:2008 production control, English documentation, a 12 month warranty and remote commissioning support are included.
Contact Person: Levi.Li
Tel: 86-13396686968
Fax: 86-574-81688011