|
Product Details:
Payment & Shipping Terms:
|
| Number_of_die_heads: | 1 / 2 / 3 / 4 | Head_centre_distance: | Adjustable On Request |
|---|---|---|---|
| Plasticizing_capacity_hdpe: | 90 Kg/h | Max_product_volume: | 10 L |
| Clamping_force: | 150 KN | Max_mould_size_w_x_h: | 520 X 460 Mm |
| Highlight: | four head bottle moulding machine,plastic extrusion molding machine,10 litre container moulding machine |
||
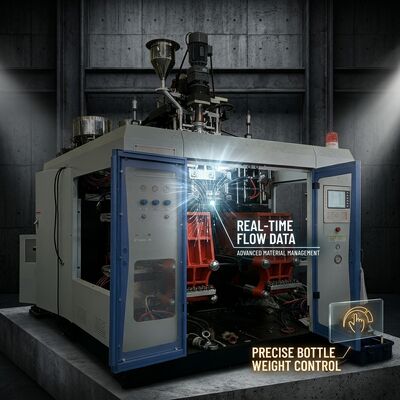
Capacity in blow moulding is rarely about the biggest machine on the floor; it is about how many finished parts leave each cycle. The MP80D is offered with a one, two, three or four head die configuration on the same 80 mm extruder, so a single machine footprint can move from prototype volumes to four-cavity production runs without a second purchase order.
Running four heads on a 90 kg/h plasticizing rate only works if the head system is thermally stable. Each die head carries three heating zones and 10 kW of dedicated power, keeping all four parisons at the same temperature and length so cavity-to-cavity weight variation stays inside the tolerance your customers audit. The 150 kN clamp then holds four cavities shut against blow pressure without the platen deflection that shows up as uneven flash on outer cavities.
Production Advantages| Parameter | Specification |
|---|---|
| Available head configurations | 1, 2, 3 or 4 heads |
| Max containers per cycle | 4 |
| Max product volume per cavity | 10 L |
| Plasticizing capacity (HDPE) | 90 kg/h |
| Mould clamping force | 150 kN |
| Max mould size (W x H) | 520 x 460 mm |
| Plate stroke | 540 mm |
| Platen opening stroke | 220-620 mm |
| Screw diameter | 80 mm |
| Total machine power | 80 kW |
Adding heads increases parts per cycle but also increases the mass of hot plastic that must be cooled before ejection. On four-cavity work with larger containers, mould cooling design rather than machine speed tends to set the cycle. Water flow of around 40 L/min at the recommended inlet temperature is specified precisely so the chiller and manifold can be sized correctly at the quotation stage.
For each project we model the intended cavity count against the 90 kg/h plasticizing ceiling. If a four-cavity mould would starve the extruder, the honest recommendation is two heads and a shorter cycle rather than four heads and perpetual waiting.
Frequently Asked QuestionsCan I add heads later instead of ordering four from the start?
Yes. The extruder, clamp and control cabinet are identical across head counts, so the machine can be upgraded with an additional head assembly and a matching mould. This is why many customers start with two heads and step up once order volume justifies it.
How much does cavity weight vary across four heads?
Cavity-to-cavity weight variation is governed by parison length and temperature uniformity. With the three-zone head heating held in steady state and moulds cut from a single tool block, variation is typically within 1-2% of nominal weight, which is inside most packaging specifications.
Will four heads reduce the maximum container size?
No, the 10 L limit applies per cavity. What changes is the practical combination: four large cavities may exceed the plasticizing rate, so large containers are usually run one or two up while small bottles are run four up.
Contact Person: Levi.Li
Tel: 86-13396686968
Fax: 86-574-81688011